Quality Assurance & Inspection
We write the inspection and test plan, qualify welding procedures and welders, and record welds, bolts and coatings against it, so your project's quality is on record.
Competencies in this capability
Each competency below is delivered under the same contract and the same quality system.
Quality Plan & ITP
We prepare the ITP with the method statement and set its inspection points. Material certificates, material lists and coating test reports are checked against it.
Welding Procedure Qualification
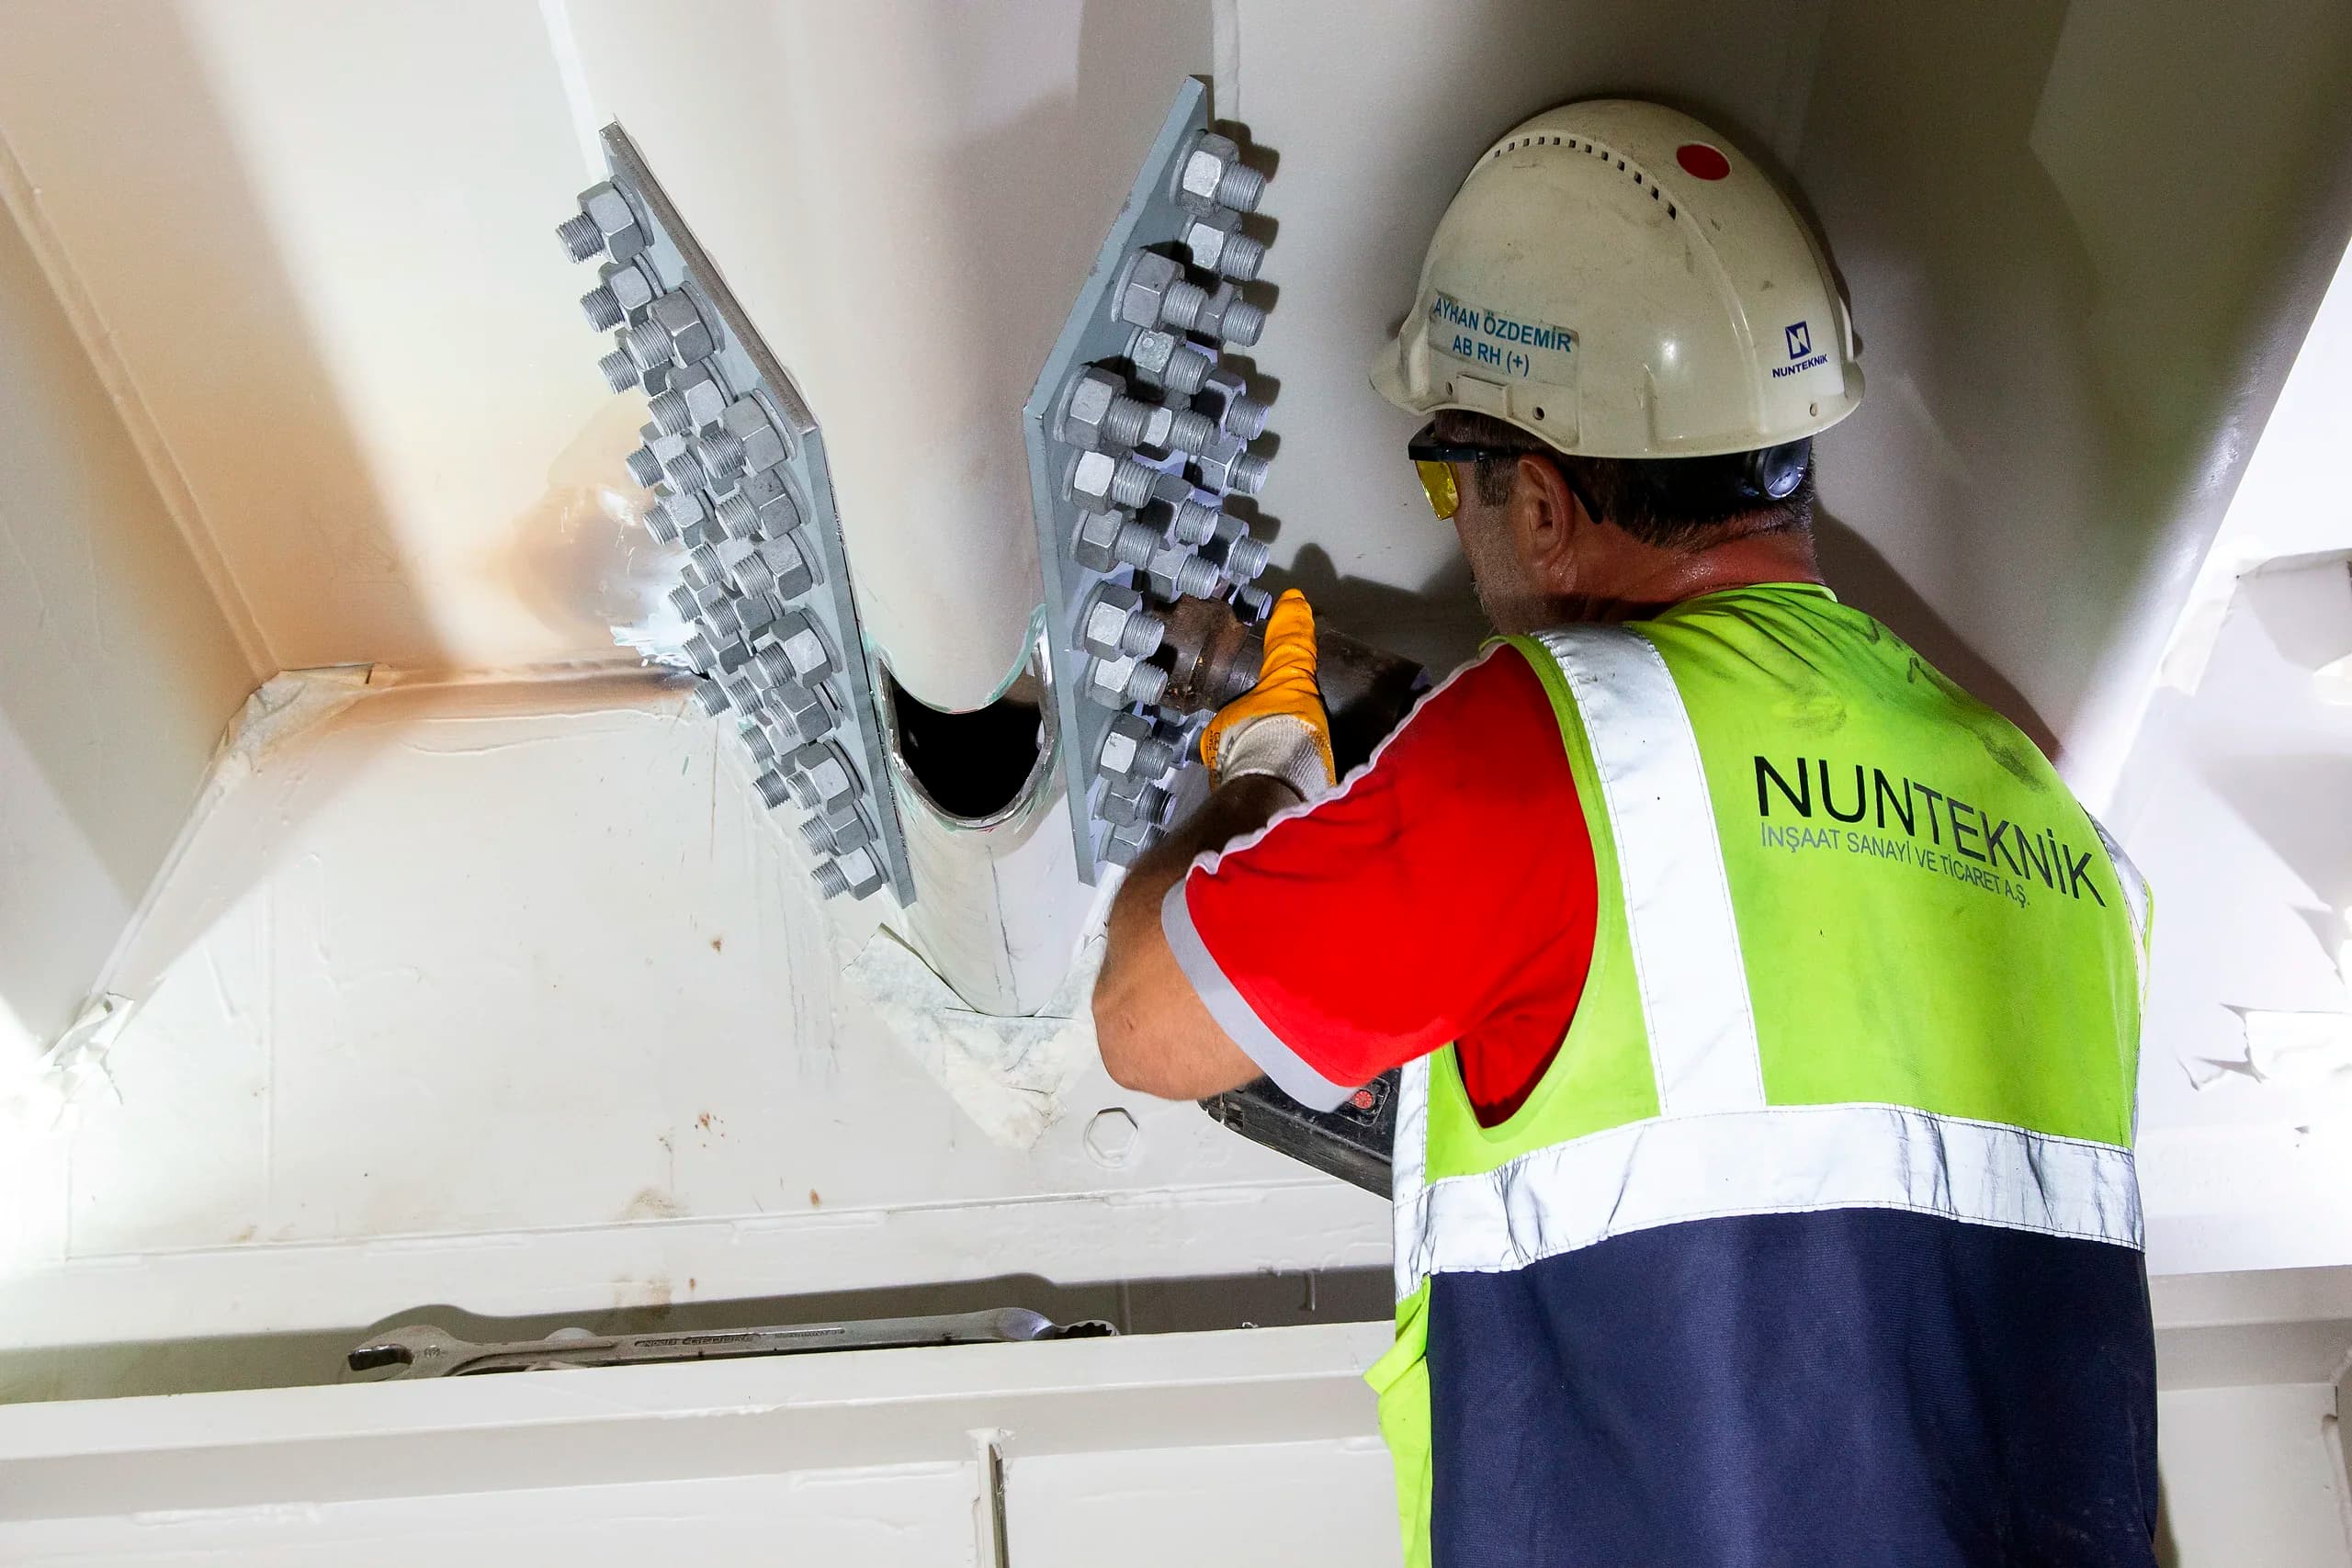
Welding procedures and welder qualifications in our name, from AASHTO/AWS D1.5 repair procedures with preheat to processes 136 and 121 on 35–50 mm S460M joints.
Third-Party Inspection
Inspection requests go to the consultant before NDT, bolt checks and painting, and MT is carried out by third-party bodies. WIR and MRIR requests track each check to closure.
Non-Destructive Testing
Visual and dimensional weld checks, then MT and UT, with dye-penetrant testing to locate crack tips. On deck repairs, NDT comes at least 24 hours after welding.
Where we applied it
Selected projects: inspection plans, welding procedures and testing
| Project | Applied as | Standard | Scale |
|---|---|---|---|
| 1915 Çanakkale Bridge Expansion Joints | ITP, own WPS, VT, MT and UT, records per joint | 4 joints | |
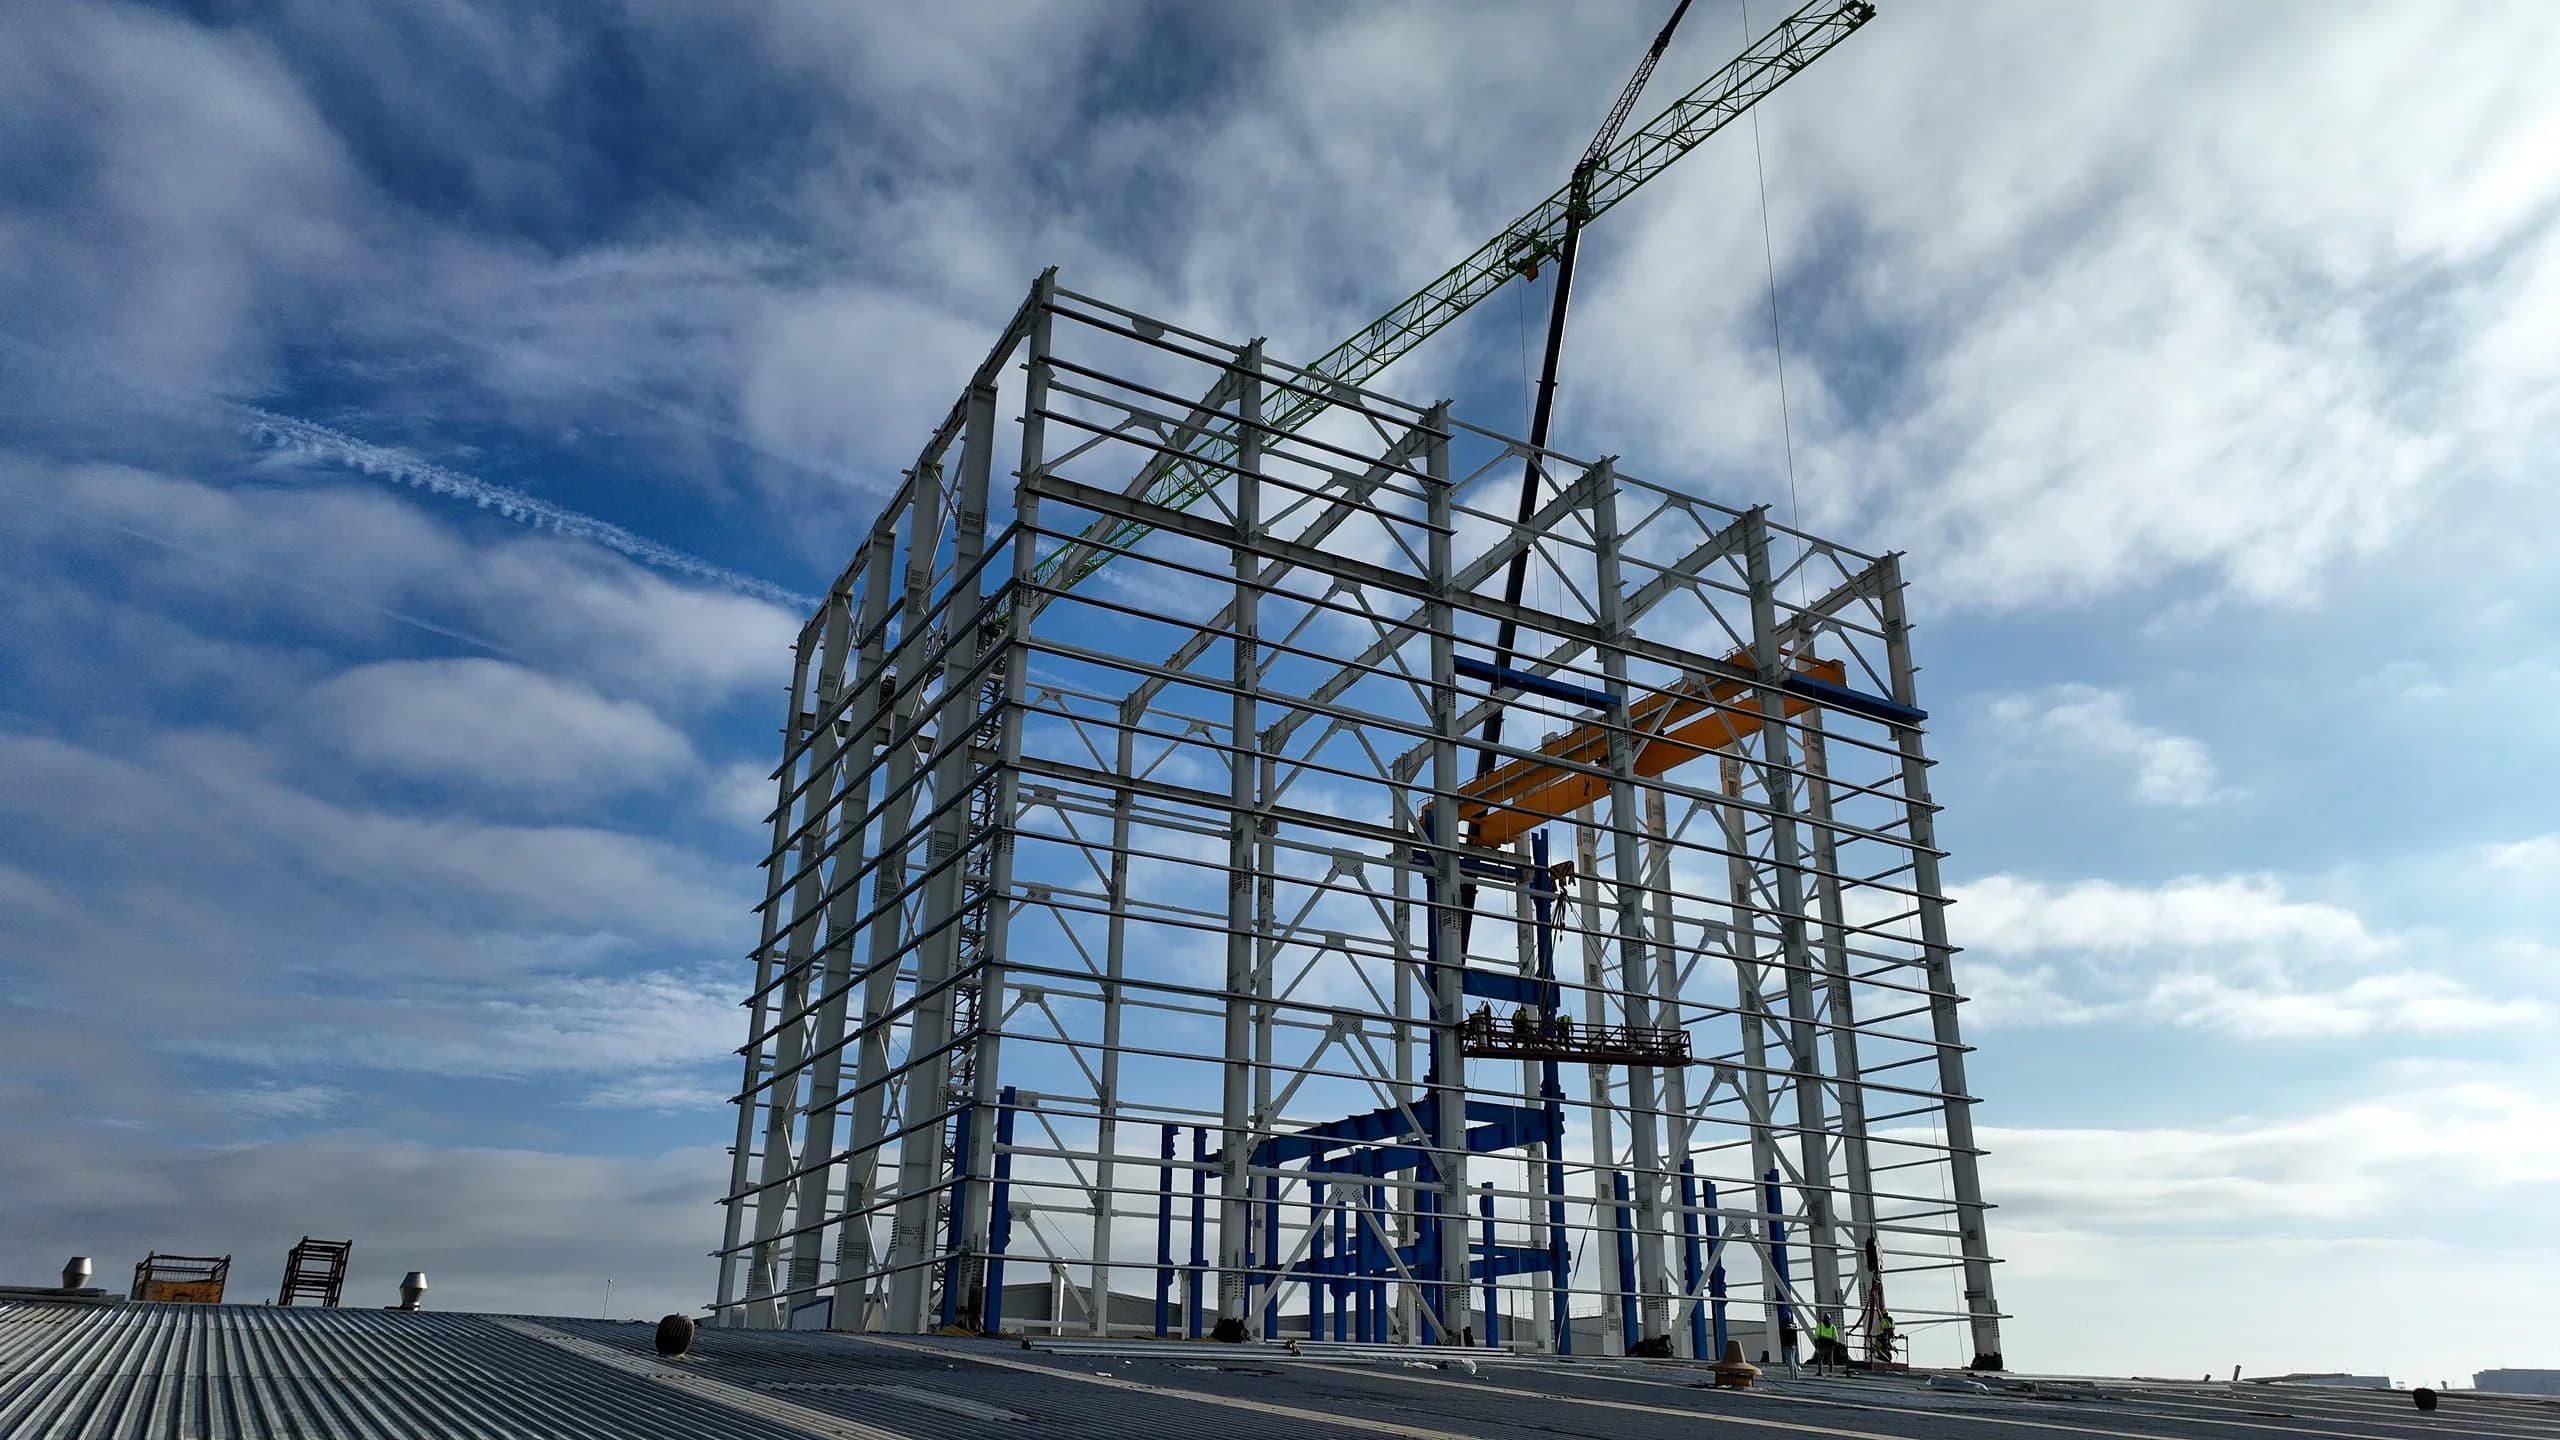
| Çorlu Steel Building and Machine Towers | ITP prepared; weld and paint reports accepted | EXC3 | around 1,093 t |
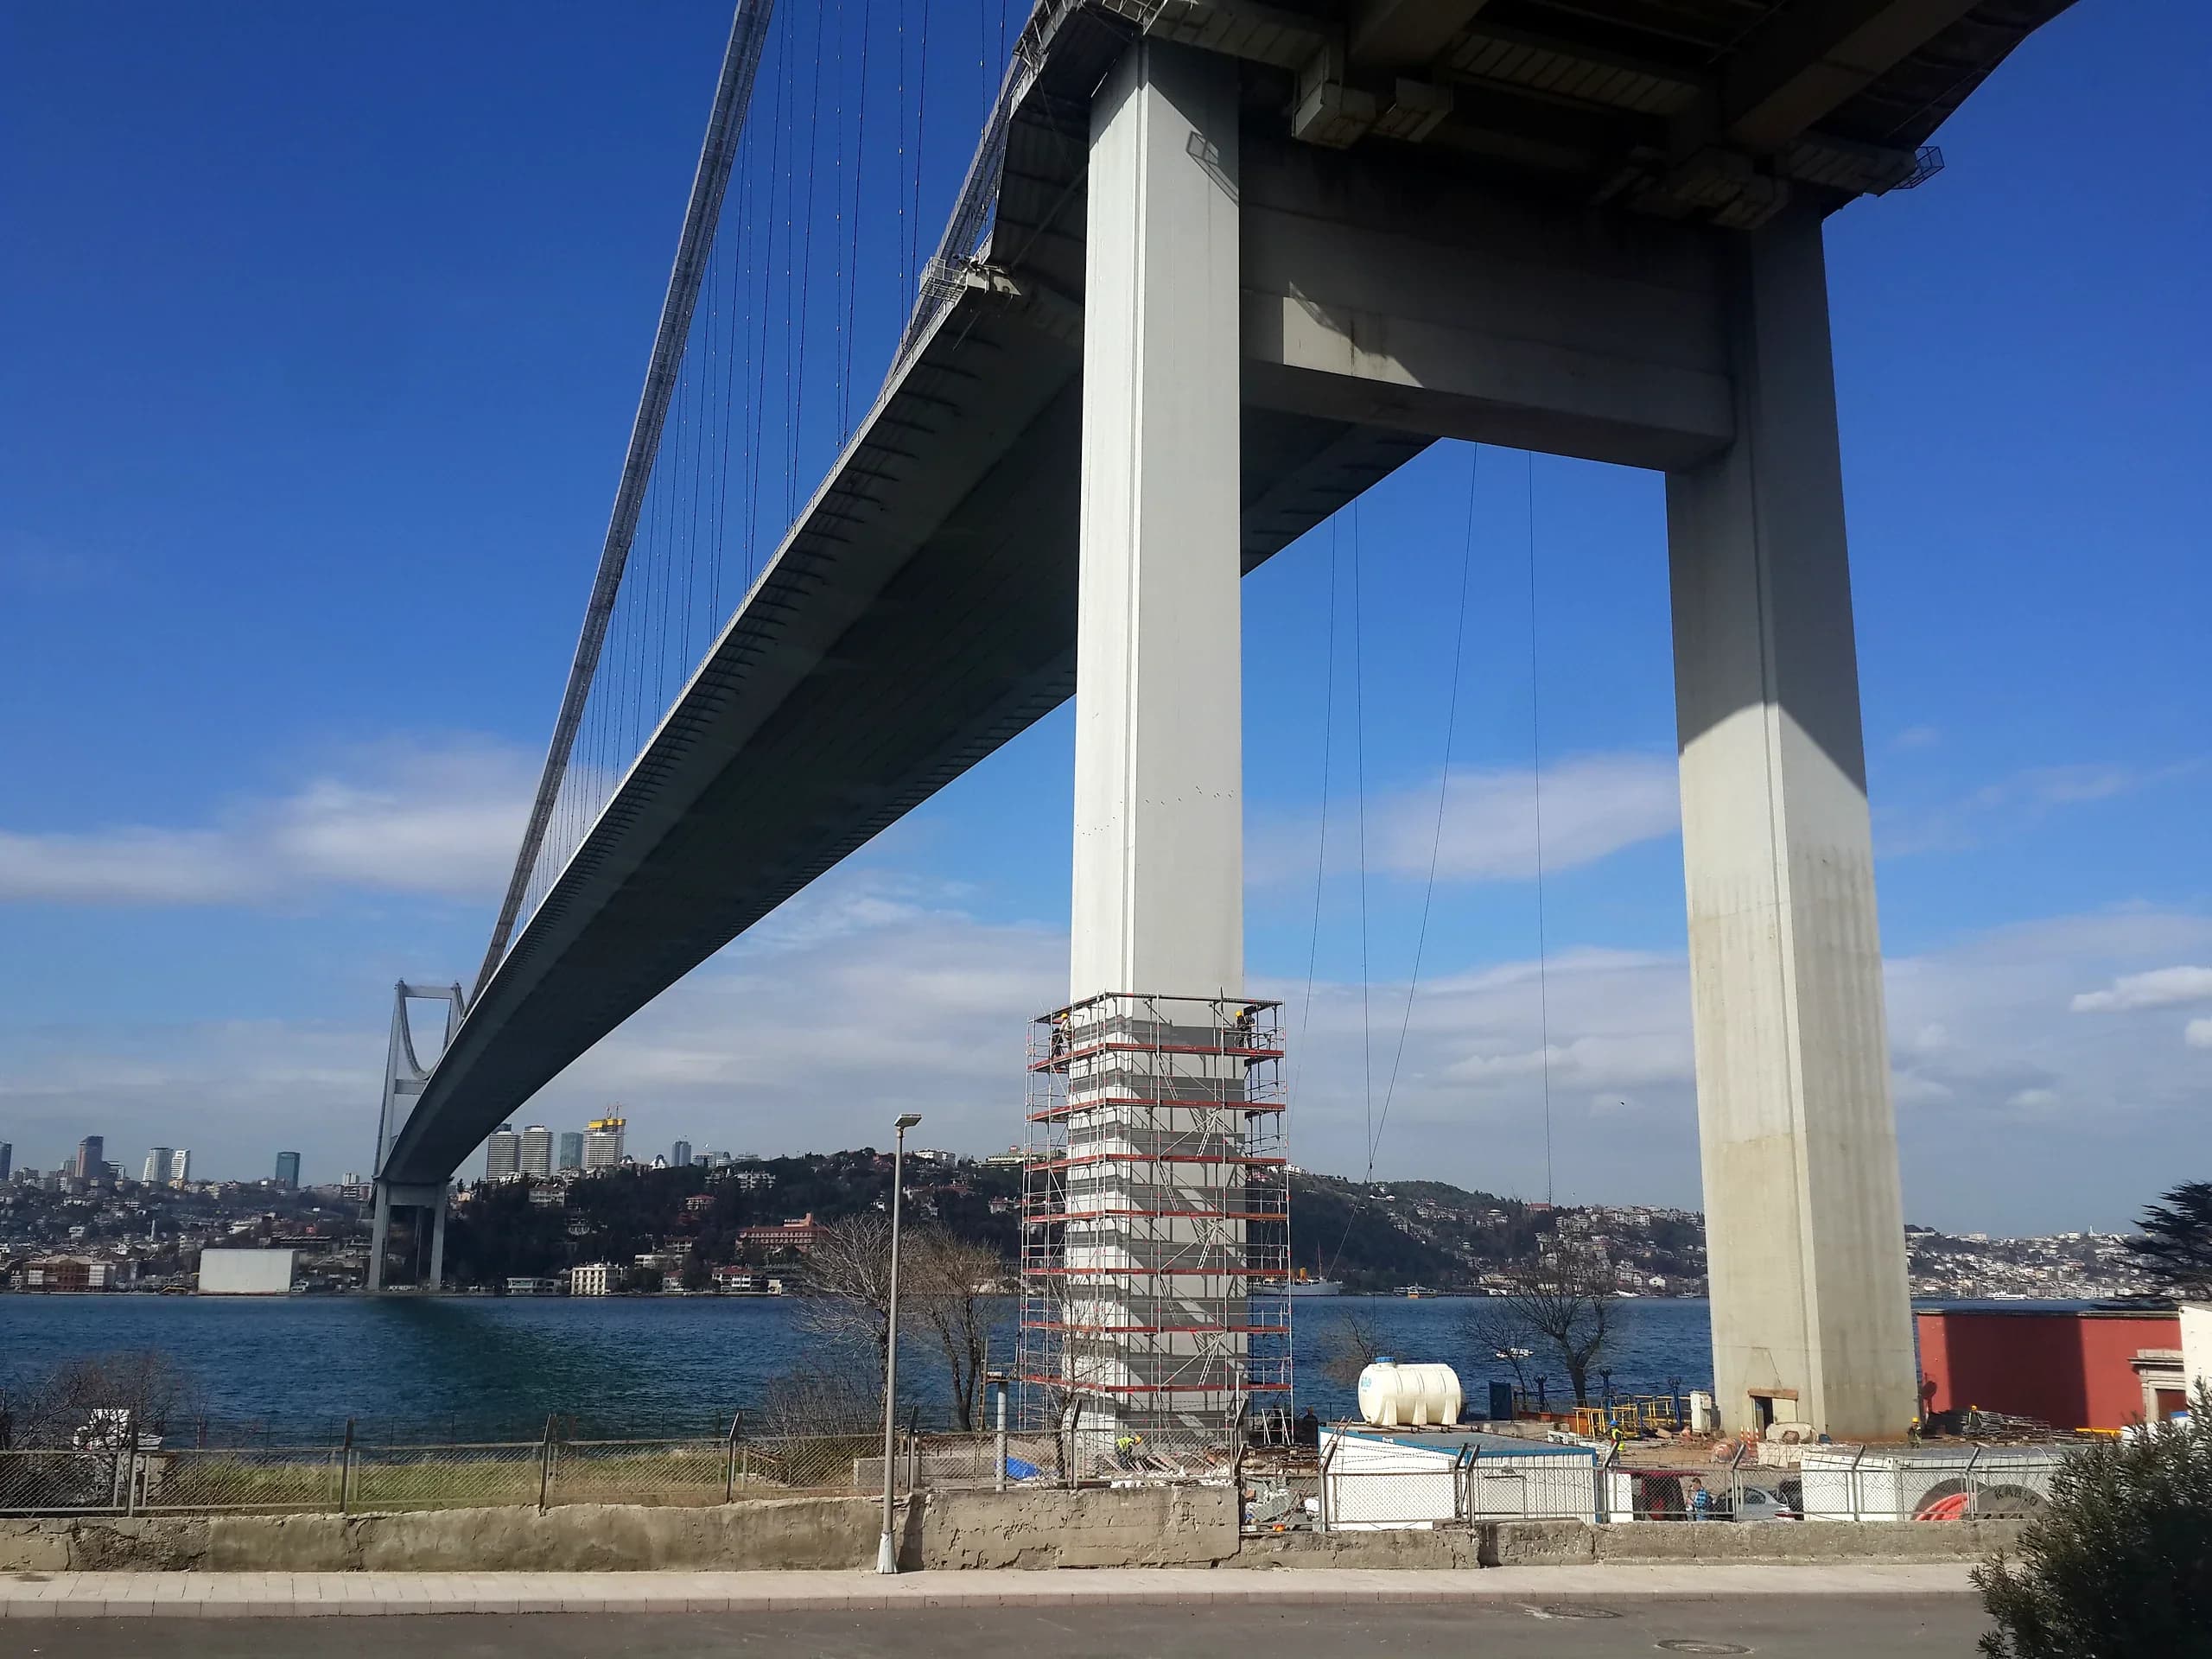
| Fatih Sultan Mehmet Bridge Fatigue Crack Repair | Welder tests, dye-penetrant testing, NDT | AASHTO/AWS D1.5 | 1,576 repairs |
| Bosphorus Bridge Tower-Deck Junction Repair | WPS, third-party MT, inspection requests | AASHTO/AWS D1.5 | 4 junctions |
| Bosphorus Bridge Orthotropic Deck Crack Repair | Third-party MT, inspection requests | 59 repairs | |
| 1915 Çanakkale Bridge Temporary Works Removal | ITP prepared, qualified welders | 8 qualified welders |
On these projects
- MT accepted every location examined on two bridge jobs
- Weld and paint test reports reviewed and found acceptable
- Fit-up, weld log, NDT and torque report for each joint
- Galvanising above TS EN ISO 1461 minimum in measured batch
Inspection documents
- Inspection and test plan (ITP)◷ pending
- Welding procedure specifications (WPS)◷ pending
- Magnetic particle testing reports◷ pending
Published as cover, contents and redacted signature pages. Full ITPs, method statements and shop drawings are not published.
From inspection plan to closed record
Five steps we follow so that the welds, bolts and coatings on your project are planned, tested and recorded.
Projects behind this capability
1915 Çanakkale Bridge Expansion Joints
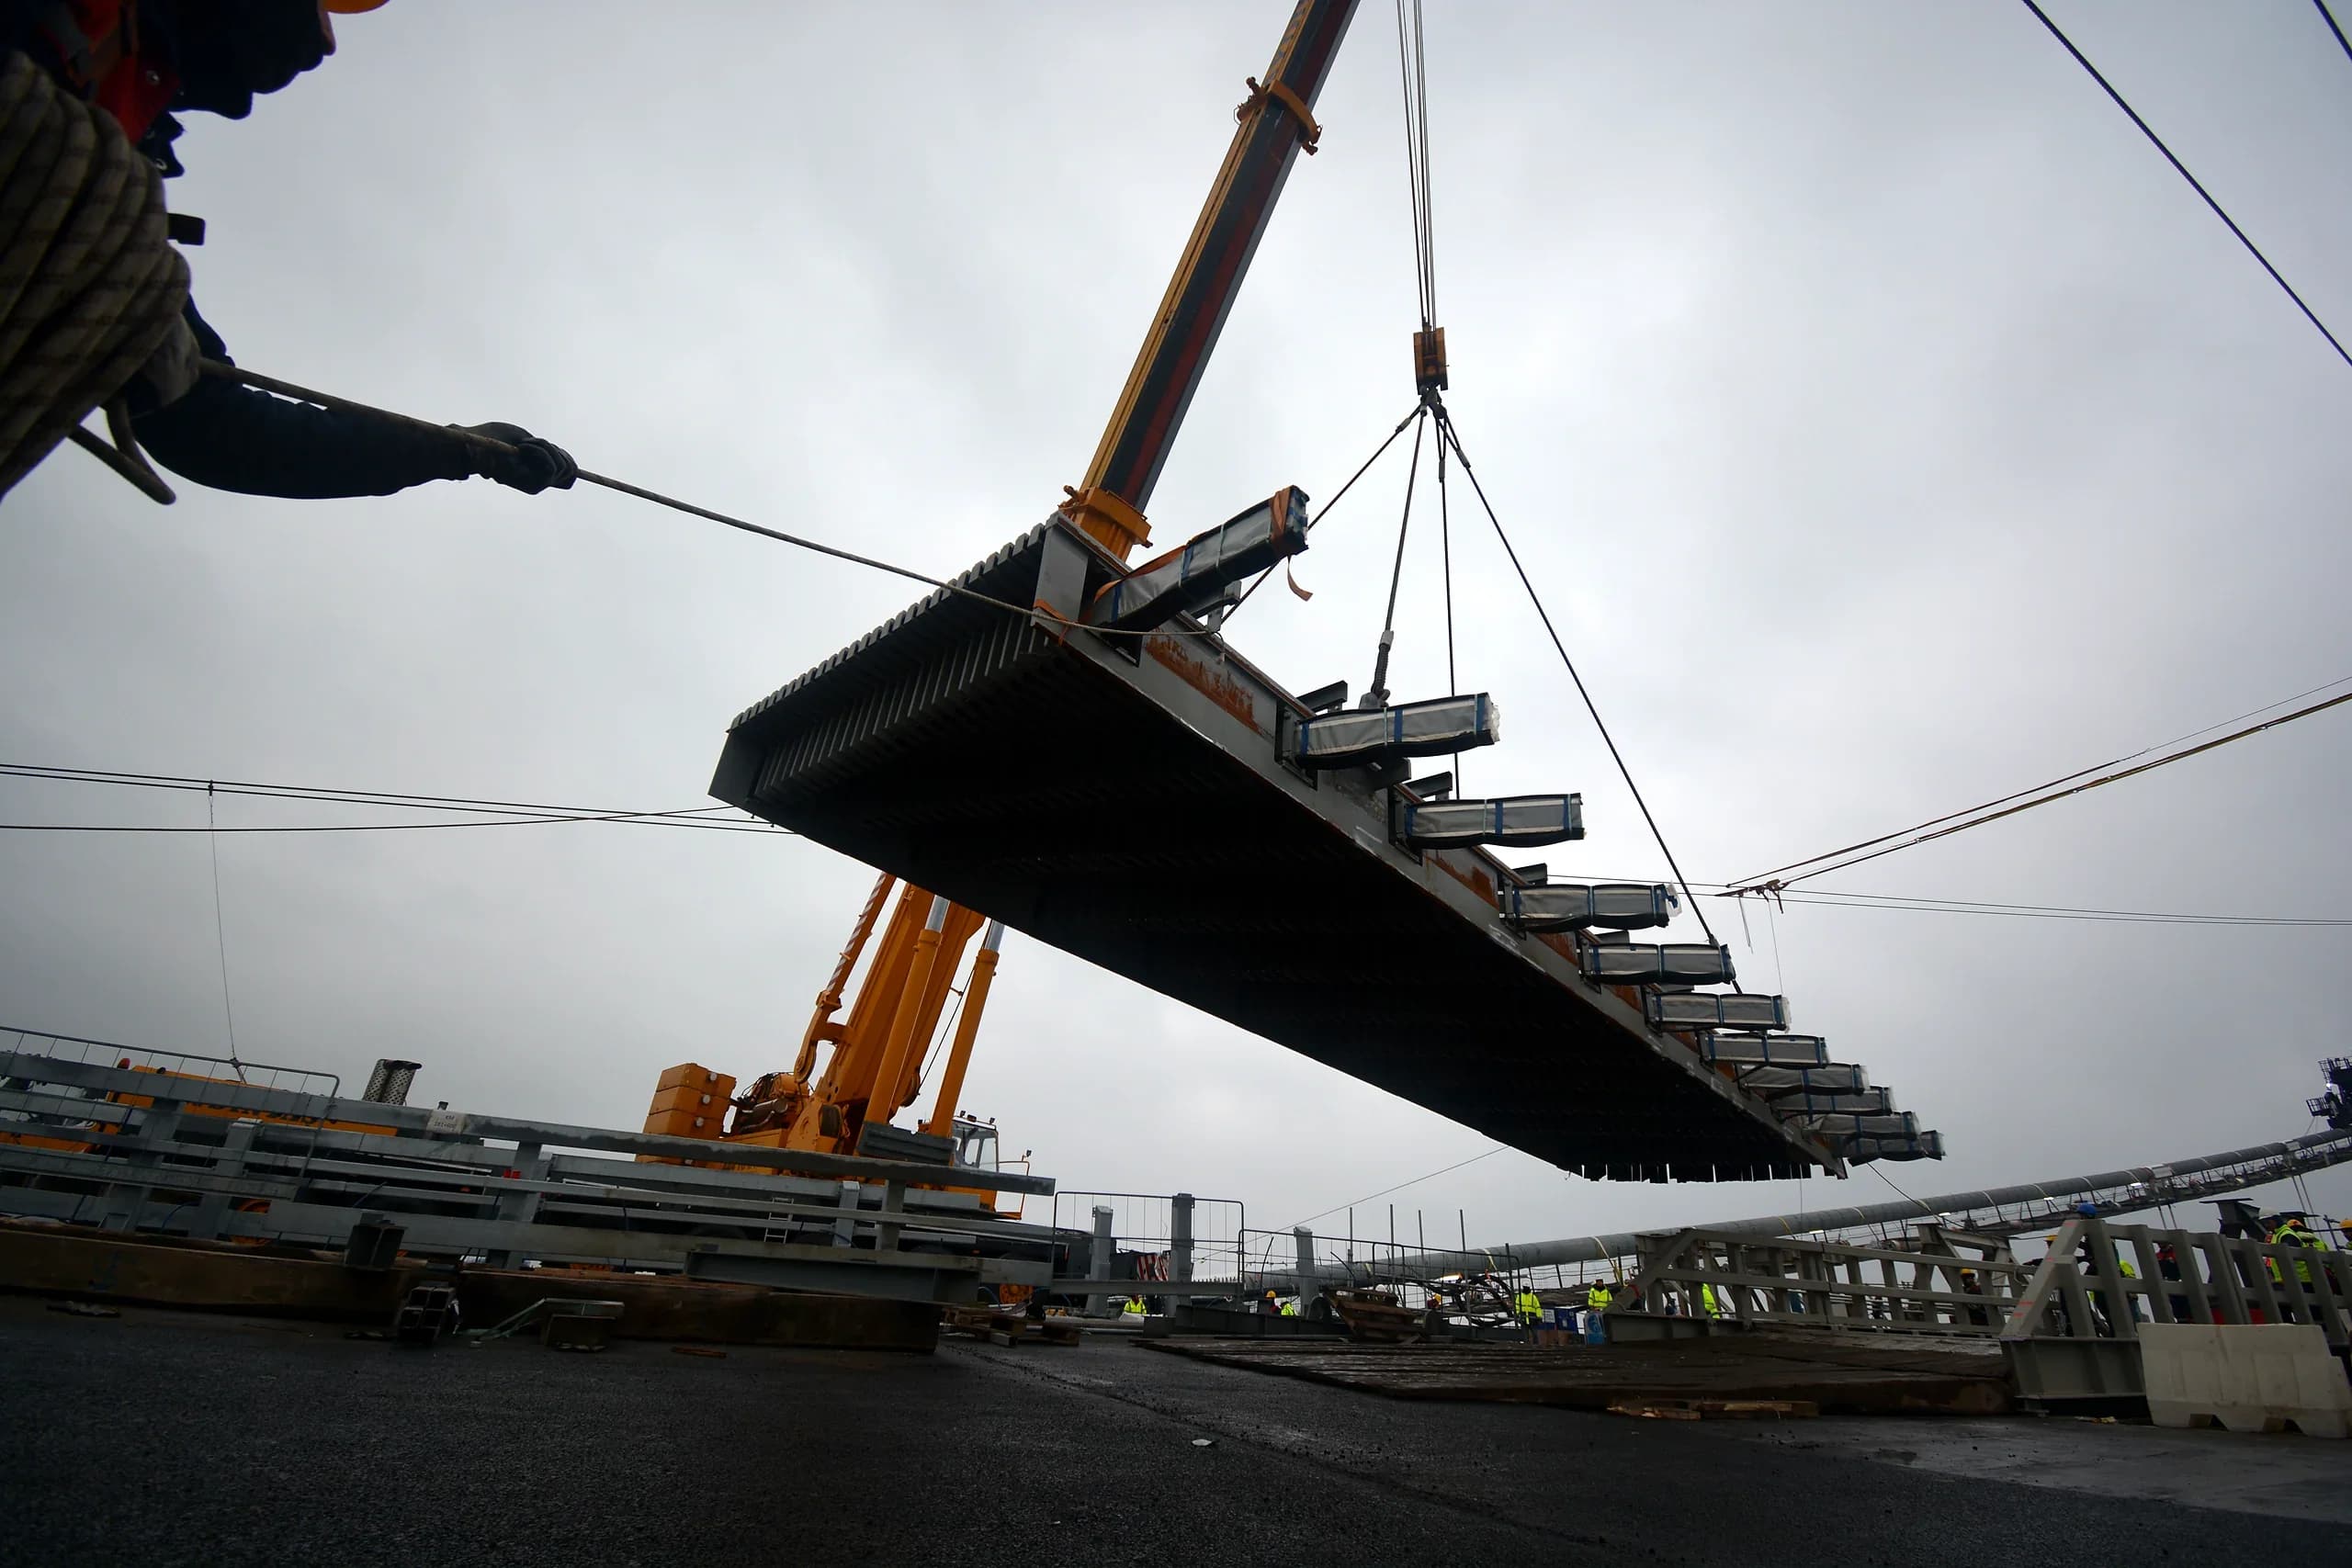
Four 55 t joints welded in 35–50 mm S460M, with fit-up, weld, NDT and torque records per joint.
Bosphorus Bridge Orthotropic Deck Crack Repair
59 fatigue cracks repaired from inside the deck; MT accepted all 19 locations examined.
Frequently asked questions
Who prepares the inspection and test plan?
We do. On the 1915 Çanakkale Bridge expansion joints and temporary works removal, and on the Çorlu steel building and towers, the ITP was prepared by Nunteknik. The Çorlu ITP set Execution Class EXC3 and EN 1090-2 Class 1 tolerances.
Do you hold your own welding procedures?
Yes. WPS and WPQR are in Nunteknik's name. On the 1915 Çanakkale Bridge we welded 35–50 mm S460M joints to our own WPS with processes 136 and 121; on the Bosphorus Bridge our WPS followed AASHTO/AWS D1.5 with 120 °C preheat.
Which NDT methods do you use?
Visual, magnetic particle and ultrasonic testing, with dye-penetrant testing to locate crack tips. On the Fatih Sultan Mehmet Bridge, dye-penetrant testing found 194 cracks beyond the contract list, and NDT came at least 24 hours after welding.
How does third-party inspection work on your sites?
We raise inspection requests to the consultant before NDT, bolt checks and painting. On two Bosphorus Bridge jobs, MT was carried out by a third-party inspection body to EN ISO 17638 and accepted every location examined.
Does subcontracted work go through the same checks?
Yes. Work by our partner shops and by the subcontractors we manage passes through our ITP and inspection chain. On the Çorlu project, the ITP control column covered both the partner shop and Nunteknik.
Let's Discuss Your Quality Plan
Send us the specification and the inspection requirements. We will set out the ITP, procedures and records we would put in place on your project.